Operational Hurdles
Industrial Drilling and Pumping Challenges in Egypt
Operators face critical efficiency losses due to abrasive materials, harsh desert environments, and equipment wear.
Rapid Component Wear
Abrasive slurry in mining operations leads to premature failure of pump liners and impellers, causing frequent unplanned downtime and increasing maintenance costs in remote Egyptian sites.
Drilling Inefficiency
Outdated borehole machine setups often struggle with Egypt's varied geological strata, leading to slow penetration rates and higher fuel consumption.
Spare Parts Scarcity
Difficulty in sourcing precise OEM-grade slurry pump parts creates bottlenecks, forcing operators to use suboptimal replacements that reduce overall system life.
Thermal Stress
Extreme ambient temperatures in North Africa place immense stress on diesel compressors and drilling rigs, leading to overheating and reduced volumetric efficiency.
Tooling Degradation
Standard dth drilling tools often wear out quickly when encountering high-hardness rock formations, increasing the cost per meter drilled.
High Operating Costs
The combination of energy-inefficient compressors and frequent part replacements drives up the total cost of ownership for municipal and petrochemical infrastructure projects.
Engineered Excellence
Integrated Solutions for Egypt's Industrial Sector
We combine advanced metallurgy with precision engineering to maximize equipment uptime and operational throughput.
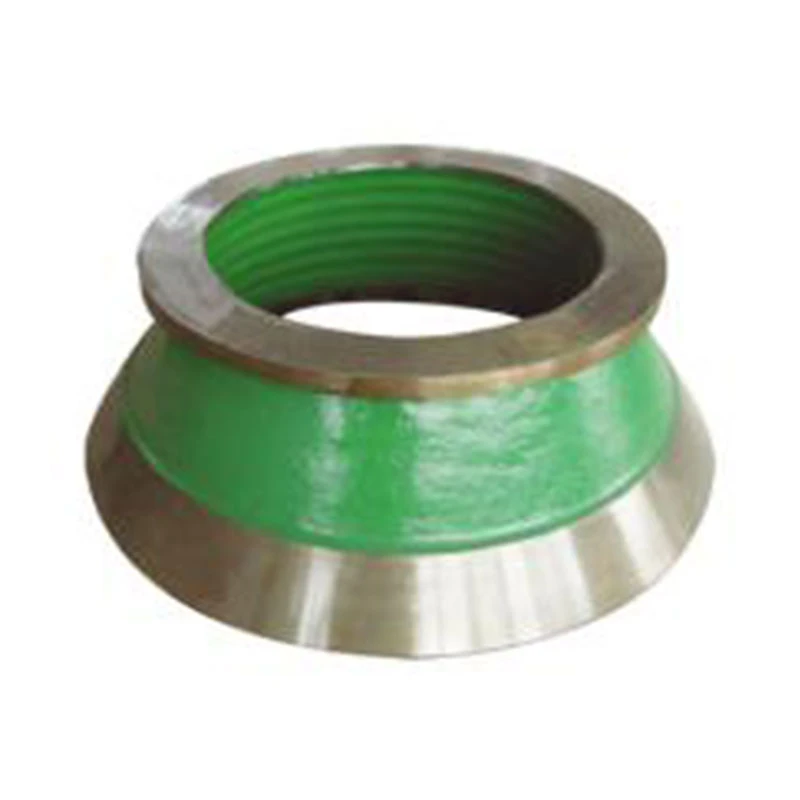
High-Chrome Alloy Castings
Using super high chrome hyper eutectic white iron, we produce wear-resistant components that significantly extend the service life of pumps handling abrasive slurry.
Precision DTH Tooling
Our downhole drilling equipment is engineered for stability and impact resistance, ensuring faster penetration in hard rock formations.
OEM Foundry Services
We provide exact-fit OEM services for pump manufacturers, delivering bimetallic and high manganese steel castings that maintain strict tolerances for seamless installation.
High-Efficiency Compressors
The diesel road compressor series features integrated monitoring and an eco-system design to maintain high pressure despite high temperatures.
Rig Renovation Services
We offer technical consultation and upgrading for DTH drilling rigs, optimizing equipment matching to reduce fuel consumption and improve drilling accuracy.
Corrosion-Resistant Materials
Specialized low carbon high chrome alloys are applied to pump models like ZGB and SP/SPR to combat the chemical corrosion found in petrochemical applications.


Production Capacity
Technical Capabilities at a Glance
Our annual output reflects our ability to support large-scale industrial projects worldwide.
0+
Whole Pump Sets Annually
0t
Alloy Castings Per Year
0+
Casting Material Types
0%
OEM Precision Match
0h
Technical Consultation
0+
Global Industry Sectors
0+
Pump Model Series
0m
Drilling Capability
Regional Analysis
Egypt's Industrial Machinery Landscape
Evaluating the intersection of resource extraction and infrastructure development in North Africa.
Egypt possesses a diverse industrial base where mining and municipal construction play pivotal roles. The geography, characterized by vast desert regions and the Nile delta, creates contrasting operational environments. Mining sectors often deal with highly abrasive sands and hard rock, necessitating heavy-duty pump and drilling equipment. Meanwhile, urban expansion in cities like Cairo and Alexandria drives demand for reliable municipal dredging and water management systems, where efficiency and reliability are the primary KPIs for equipment procurement.
Current market trends indicate a shift toward "life-cycle cost" optimization. Instead of purchasing the cheapest initial equipment, Egyptian firms are increasingly investing in high-chrome alloys and precision-engineered spare parts to reduce the frequency of maintenance. The integration of diesel-powered compressed air solutions with comprehensive monitoring is also becoming standard, allowing operators to maintain high pressure in remote locations without sacrificing fuel economy or equipment longevity.
The outlook for the Egyptian market is shaped by large-scale national infrastructure projects and a growing focus on petrochemical efficiency. However, constraints such as extreme heat and the abrasive nature of local soils remain constant. The opportunity lies in providing specialized, wear-resistant materials and three-dimensional drilling solutions that can adapt to these specific geological conditions, moving away from generic equipment toward application-specific engineering.
Industry Progress
Evolution of Pumping and Drilling Technology
From basic iron castings to advanced hyper-eutectic alloys and integrated air solutions.
Early Phase
Basic Metallurgy
Reliance on standard cast iron and basic diesel rigs, characterized by high failure rates in abrasive conditions and limited depth capabilities.
Growth Phase
Alloy Optimization
Introduction of high-chrome white iron and bimetallic castings, which significantly improved wear resistance and expanded the use of slurry pumps.
Current Phase
Integrated Systems
Transition to comprehensive solutions including DTH rig upgrades, eco-friendly compressors, and customized 3D drilling consultation.
Material Science Shift
The move toward super high chrome hyper eutectic white iron represents a critical leap in durability. By optimizing the carbon and chromium balance, components can now withstand extreme abrasion that would destroy standard alloys in weeks.
Precision OEM Standardization
The industry is moving away from "approximate fits" to strict OEM tolerances. This ensures that spare parts for G/GH gravel pumps or AH series pumps integrate perfectly, eliminating installation leaks and vibration.
Digital Monitoring Integration
Modern air compressors now include integrated monitoring systems that allow operators to track performance and schedule preventative maintenance, reducing the risk of catastrophic failure in the field.
Future Outlook
Key Trends in Heavy Equipment Manufacturing
Analyzing the technological drivers shaping the next generation of industrial machinery.
Hybrid Energy Power-trains
Transitioning from pure diesel to hybrid-electric compressors to lower emissions and fuel costs while maintaining high pressure for DTH drilling.
AI-Driven Wear Prediction
Utilizing sensor data to predict when slurry pump liners will fail, allowing for "just-in-time" replacement of spare parts.
Ultra-Hard Surface Coating
Applying nano-ceramic coatings to DTH drilling tools to further reduce friction and extend tool life in granite and basalt.
Modular Equipment Design
Developing pumps and rigs with modular components to allow for rapid on-site upgrades and reduced transportation logistics.
The overarching trend is the transition from selling a product to providing a "total uptime solution." For Egyptian operators, this means the value is no longer just in the borehole machine itself, but in the accompanying technical consultation and the availability of high-chrome alloy castings that ensure the machine stays operational during peak production cycles. This holistic approach reduces the risk of costly project delays.
Furthermore, environmental regulations are beginning to influence the design of diesel air compressors. There is a clear move toward "Eco-system" integrated designs that optimize combustion and noise levels without sacrificing the high-pressure capacity required for deep-hole drilling. These advancements are essential for companies operating in municipal construction zones where noise and emission constraints are more stringent than in open-pit mining.
Practical Applications
Implementation Scenarios in Egypt
How our technology solves real-world industrial problems across different Egyptian sectors.
01
Mining Site in the Eastern Desert: Abrasive Slurry Management
In the Eastern Desert, mining operators handle high-density mineral slurries. The combination of extreme heat and abrasive particles rapidly eroded standard pump impellers. By deploying ZGB type slurry pumps with super high chrome white iron castings, the operation reduced pump failure rates and extended the interval between impeller replacements from weeks to months, ensuring stable ore transport.
02
Cairo Municipal Construction: Efficient Water Well Drilling
Urban expansion requires rapid installation of water boreholes. Using our borehole machine integrated with DTH drilling tools, contractors were able to penetrate varied soil layers more efficiently. The high-pressure diesel road compressors provided a stable air supply, reducing the total drilling time per well and minimizing disruption to city traffic.
03
Suez Canal Industrial Zone: Petrochemical Fluid Transport
In the petrochemical plants near Suez, pumps must handle corrosive fluids alongside abrasive particles. Operators implemented M/AH/HH pump models with corrosion-resistant low carbon alloys. This technical choice prevented the pitting and chemical degradation common in standard steel pumps, significantly increasing the safety and reliability of fluid transport lines.
04
Nile Delta Dredging: Silt and Gravel Removal
Dredging operations in the Nile Delta often encounter a mix of fine silt and coarse gravel. Using G/GH gravel pumps with OEM-fit frame plate liners, the dredging fleet achieved higher volumetric efficiency. The wear-resistant materials ensured that the pumps could handle the diverse particle sizes without clogging or rapid internal erosion.
05
Remote Infrastructure Project: Rig Upgrading and Maintenance
A remote construction project struggled with declining drilling speeds due to aging rigs. Through our technical consultation and DTH rig renovation services, the equipment was matched with upgraded drilling tools and optimized air systems. This renovation restored the rigs to factory-level efficiency, reducing fuel costs and improving the precision of foundation piling.
Operational Feedback
Representative Operator Perspectives
Illustrative scenarios demonstrating the impact of high-chrome alloy and drilling solutions.
In abrasive mining environments, the transition to super high chrome alloy pump parts has been a game-changer. We observed a significant reduction in unplanned downtime compared to standard alloy components, allowing us to maintain a consistent production schedule despite the harsh geological conditions found in the desert.
Upgrading our DTH drilling tools and matching them with high-pressure diesel compressors improved our penetration rates in hard rock formations. The ability to get precise OEM-grade replacements quickly ensures that our municipal projects stay on track without waiting weeks for custom-machined parts.
The technical consultation for rig renovation helped us identify inefficiencies in our air supply system. By integrating a more reliable diesel compressor and optimizing the downhole tools, we reduced our fuel consumption per meter drilled while increasing the overall stability of the borehole.
Our Heritage
About Zen Young Technology Hebei Co., Ltd.
A specialized provider of slurry pump solutions, foundry OEM services, and advanced drilling equipment.
Foundational Capacity
Specialization in Slurry Solutions
Established as a specialist in slurry pump solutions and foundry OEM services, focusing on high-wear environments across mining, metallurgy, and petrochemical industries.
Technical Expansion
Drilling and Compression Integration
Expanded capabilities to include three-dimensional drilling solutions, DTH drilling rigs, and full-range compressed air solutions for global industrial applications.
Scale Optimization
High-Volume Advanced Casting
Achieved a production scale of over 5,000 whole pump sets and 10,000 tons of high chrome alloy castings annually, supporting various wear-resistant materials.


Expert Advice
Industrial Equipment Frequently Asked Questions
Technical answers to help Egyptian operators select the right pumps and drilling tools.
What is the primary advantage of high-chrome alloys in slurry pump parts?
High-chrome alloys, particularly super high chrome hyper eutectic white iron, provide exceptional hardness and abrasion resistance. In slurry pumps, this means the impellers and liners can withstand the constant impact and scrubbing of abrasive minerals. For operators, this translates to a significantly longer service life and reduced frequency of part replacements compared to standard manganese steel or cast iron.
How do I choose the right DTH drilling tools for hard rock in Egypt?
Selection depends on the rock's compressive strength and abrasiveness. For extremely hard formations like granite, we recommend high-grade carbide inserts with a specific face geometry to optimize penetration. It is also critical to ensure the tools are matched with a compressor that provides the correct CFM and pressure to clear cuttings efficiently from the borehole, preventing tool sticking and overheating.
Can Zen Young provide OEM parts for existing pump brands?
Yes, we specialize in Foundry OEM services. We can produce replacement parts for a wide range of models, including ZGB, G/GH, M/AH/HH, and SP/SPR pumps. By utilizing precision machining and advanced casting techniques, we ensure that our OEM parts match the original specifications for fit and function, often improving upon the original wear resistance through the use of superior alloy materials.
What considerations are necessary for diesel compressors in desert climates?
The main considerations are cooling efficiency and air filtration. In desert environments, high ambient temperatures can lead to overheating, while fine sand can clog filters and damage internals. Our diesel road compressors feature integrated monitoring and an overall integrated design that optimizes heat dissipation and air intake, ensuring consistent high-pressure output even in extreme North African heat.
What is the benefit of "three dimensional drilling solutions" over basic equipment?
Three dimensional solutions move beyond just providing a machine; they encompass equipment matching, on-site technical services, and rig renovation. This approach ensures that the compressor, rig, and drilling tools are perfectly synchronized. The result is optimized energy use, faster penetration rates, and a reduction in tool wear, which lowers the overall cost per meter drilled for the operator.
How do I start the process of upgrading my existing drilling rig?
The first step is a technical consultation where we analyze your current equipment's performance and the specific geology of your site. We then provide a renovation plan that may include upgrading DTH drilling tools, optimizing the air compressor capacity, or improving the rig's mechanical efficiency. This customized approach ensures you get the maximum performance increase with the most cost-effective investment.
Get Expert Support
Optimize Your Industrial Pumping and Drilling Operations in Egypt
Whether you are managing a mining site in the Eastern Desert or a municipal project in Cairo, the right equipment and materials make the difference between profitability and downtime. Contact us to discuss custom OEM slurry pump parts or comprehensive drilling solutions tailored to your specific geological needs in Egypt.
Discuss Your Requirements
Zen Young Technology Hebei Co., Ltd. Specialized in Slurry pump solutions, Foundry OEM services, Drilling rigs and drilling tools, and Air compressors for world wide industries of mining, metallurgy, municipal construction, power, dredging, petrochemical, etc.
Copyright © 2026 Zen Young Technology Hebei Co.,Ltd. All Rights Reserved. Sitemap | Privacy Policy | Top Blog | Global Service | Hot Products | Knowledge