In the demanding landscape of industrial fluid management, finding a reliable centrifugal slurry pump manufacturer is essential for maintaining operational efficiency in mining and construction. These specialized pumps are engineered to handle abrasive materials that would quickly destroy standard pumping equipment, making them a cornerstone of heavy-duty industrial infrastructure. Understanding the nuances of pump selection and manufacturing quality ensures that enterprises can minimize downtime and maximize throughput in the harshest environments.
Globally, the demand for robust material handling solutions has surged as mining operations move toward deeper and more remote locations. The role of a professional centrifugal slurry pump manufacturer extends beyond simple fabrication; it involves precise metallurgical engineering to combat wear and erosion. By integrating advanced materials and optimized hydraulic designs, these manufacturers provide the tools necessary to transport tailings, ore slurries, and chemical wastes across vast industrial complexes.
For organizations seeking to optimize their pneumatic and fluid systems, partnering with an experienced centrifugal slurry pump manufacturer ensures a synergy between power and durability. While the industry often focuses on raw capacity, the true value lies in the longevity of the components and the ease of maintenance provided by expert design. Whether integrated with portable power sources or fixed installations, these systems drive the productivity of modern resource extraction.
The Role of a Centrifugal Slurry Pump Manufacturer in Modern Mining
A centrifugal slurry pump manufacturer serves as the primary architect for the arteries of a mining operation. By designing pumps that can move thick, abrasive mixtures of solids and liquids, they enable the efficient transport of materials from the extraction point to the processing plant. This process is critical for maintaining a continuous flow of production, as any failure in the pumping system can lead to costly site-wide shutdowns.
Beyond the hardware, these manufacturers provide the technical expertise required to calculate the precise flow rates and pressure requirements for specific slurry densities. This ensures that the equipment is neither under-specified—leading to premature failure—nor over-specified, which would result in unnecessary energy expenditure. The synergy between theoretical fluid dynamics and practical manufacturing is what defines a market leader in this sector.
Engineering Excellence and Material Durability
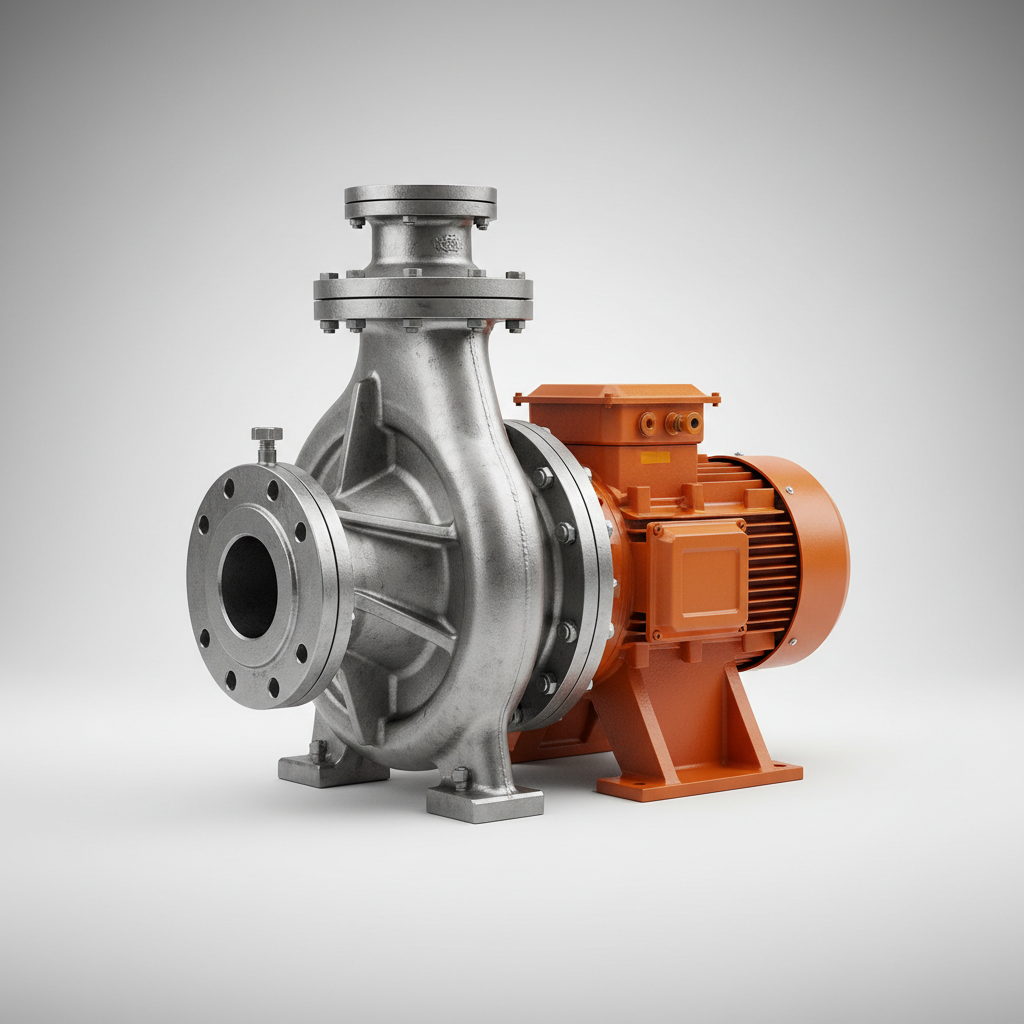
The core challenge addressed by a centrifugal slurry pump manufacturer is the extreme abrasiveness of the fluids being transported. To combat this, engineering teams focus on the selection of high-chrome alloys and specialized rubber linings that can withstand constant friction and impact. This commitment to material science ensures that the impeller and volute maintain their geometric integrity over thousands of operating hours.
Precision casting plays a pivotal role in achieving the necessary hardness and toughness. By controlling the cooling rates and chemical compositions of the metal castings, manufacturers can create components that resist both corrosive chemicals and physical wear. This dual-protection approach is vital for pumps operating in acidic mining environments or handling sharp mineral fragments.
Furthermore, the focus on modularity allows for rapid replacement of wear parts. A top-tier manufacturer ensures that the design permits easy access to the internal components, reducing the mean time to repair (MTTR). This focus on maintainability transforms the pump from a potential point of failure into a reliable asset with a predictable lifecycle.
Operational Efficiency and Design Optimization
Operational efficiency begins with the hydraulic profile of the pump. A skilled centrifugal slurry pump manufacturer optimizes the impeller vanes to reduce turbulence and prevent the settling of solids within the pump casing. This optimization not only increases the volume of material moved per kilowatt of energy but also significantly reduces the internal wear caused by erratic fluid flow.
Integrating smart monitoring systems is another area where a centrifugal slurry pump manufacturer adds immense value. By incorporating vibration sensors and pressure transducers, operators can detect early signs of cavitation or impeller wear. This shift toward predictive maintenance allows for scheduled interventions, preventing catastrophic failures that could jeopardize site safety and production quotas.
The balance between pump speed and slurry concentration is a delicate science. Manufacturers provide comprehensive performance curves that allow engineers to select the optimal operating point. When a pump operates within its best efficiency point (BEP), the longevity of the seals and bearings is maximized, ensuring the lowest possible total cost of ownership over the equipment's lifespan.
Performance Benchmarks in Slurry Transport
Evaluating the success of a slurry system requires a rigorous look at performance benchmarks. A centrifugal slurry pump manufacturer typically measures success through the lens of "wear-life" and "volumetric efficiency." These metrics determine how long the pump can operate before requiring a liner change and how effectively it moves the targeted solids concentration without clogging.
To provide a clear comparison, manufacturers often benchmark different impeller materials and designs against standard industry requirements. By analyzing the trade-off between initial cost and operational lifespan, companies can make informed decisions based on the specific chemistry and grit size of their slurry.
Efficiency Ratings by Centrifugal Slurry Pump Manufacturer Material Types
Global Applications Across Remote Industrial Zones
The application of high-performance pumps extends far beyond traditional mines. In remote industrial zones, such as the oil sands of Canada or the iron ore fields of Australia, the equipment provided by a centrifugal slurry pump manufacturer is indispensable. These regions often lack established infrastructure, requiring pumps that can be easily transported and commissioned in the field without extensive specialized tooling.
Furthermore, these systems are critical in environmental remediation and dredging projects. Whether removing contaminated silt from a riverbed or managing tailings ponds to prevent ecological leakage, the ability to move heavy solids reliably is a matter of environmental safety. The versatility of these pumps allows them to transition from mining tasks to civil engineering projects with minimal reconfiguration.
Integration with Portable Power and Air Systems
In many field operations, the slurry pump does not act alone but is part of a larger ecosystem of machinery. The integration with portable power sources, such as diesel-driven screw air compressors, allows for a fully autonomous work site. This portability is essential for emergency repair tasks and road maintenance where electrical grids are unavailable, ensuring that the pumping of debris and fluids can continue uninterrupted.
A seamless interface between the pump and its power source is a hallmark of a sophisticated industrial setup. For example, the use of high-capacity tanks and robust diesel engines ensures that the system can operate for more than 8 hours continuously. This reliability reduces the need for frequent refueling and allows operators to focus on the task at hand rather than equipment maintenance.
The synergy is further enhanced by user-friendly control panels and "gull wing" designs that allow for rapid service. When a centrifugal slurry pump manufacturer considers the entire operational environment, they create a system that is not just a pump, but a comprehensive material handling solution. This holistic approach minimizes the friction between different pieces of equipment, maximizing overall site productivity.
Future Trends in Abrasive Fluid Management
The future of slurry transport is being shaped by the digital transformation of the manufacturing sector. A forward-thinking centrifugal slurry pump manufacturer is now incorporating IoT (Internet of Things) sensors directly into the pump casing. These sensors provide real-time data on wall thickness and flow velocity, allowing for "just-in-time" part replacement and eliminating the guesswork associated with manual inspections.
Sustainability is also becoming a core driver of innovation. There is a growing shift toward energy-efficient motors and the use of recyclable composite materials for pump liners. By reducing the carbon footprint of the pumping process and extending the life of the components, manufacturers are helping mining companies meet stricter global ESG (Environmental, Social, and Governance) targets.
Finally, the rise of automation and remote-controlled mining is pushing pumps toward full autonomy. Future systems will likely feature self-adjusting impellers that change speed and pitch based on the real-time density of the slurry. This level of intelligence will virtually eliminate the risk of blockage and optimize energy consumption to an unprecedented degree.
Analysis of Material and Design Factors in Slurry Pump Performance
| Material Type |
Wear Resistance Score |
Corrosion Resistance |
Typical Application |
| High Chrome Alloy |
9.5 |
Moderate |
Hard Rock Mining |
| Natural Rubber |
7.0 |
High |
Acidic Tailings |
| Polyurethane |
8.2 |
High |
Fine Sand Slurry |
| Ceramic Lining |
9.8 |
Very High |
Chemical Processing |
| Hardened Steel |
6.5 |
Low |
General Construction |
| Hybrid Composite |
8.8 |
Moderate |
Mixed Mineral Waste |
FAQS
When selecting a manufacturer, evaluate their expertise in metallurgical casting and their ability to provide customized impeller designs. Check for a track record of durability in environments similar to your own, and ensure they offer a comprehensive range of wear-resistant spare parts for quick replacement to minimize downtime.
Rubber-lined pumps are superior for handling fine particles and corrosive chemicals, as the elastomer absorbs impact. Chrome-alloy pumps are designed for coarse, highly abrasive solids like crushed ore, where hardness is required to prevent the surface from being etched or gouged by larger particles.
Replacement intervals vary based on the slurry's abrasiveness and the pump's operating speed. However, implementing a predictive maintenance schedule using vibration analysis or wall-thickness testing is recommended. Most high-quality manufacturers suggest a quarterly inspection to prevent catastrophic impeller failure.
Yes, provided the pump is correctly sized. A professional manufacturer will design the pump to maintain a "critical velocity," which ensures that solids remain suspended in the fluid and do not settle in the pipe or casing, which would otherwise cause a blockage.
Absolutely. Many operations use diesel-driven systems for flexibility in remote areas. Ensuring that the power source can provide consistent torque and that the system includes a robust cooling mechanism is key to maintaining the pump's performance in harsh, off-grid environments.
Common signs include an increase in vibration, a drop in discharge pressure, or an unusual increase in energy consumption for the same flow rate. These often indicate internal wear or cavitation, signaling that it is time to consult your manufacturer for a parts overhaul.
Conclusion
Selecting a partner from the pool of centrifugal slurry pump manufacturer options is more than a procurement decision; it is a strategic investment in operational stability. By focusing on material science, hydraulic optimization, and the integration of portable power, industries can ensure that their material handling systems are resilient against the most aggressive environments. The balance of durability and efficiency remains the gold standard for success in mining and industrial construction.
Looking ahead, the integration of AI-driven monitoring and sustainable materials will further redefine the capabilities of slurry transport. Organizations that adopt these innovations early will gain a significant competitive advantage through reduced operating costs and enhanced environmental compliance. For those seeking world-class pumping and air compression solutions, we invite you to explore our professional range. Visit our website: www.miningzy.com